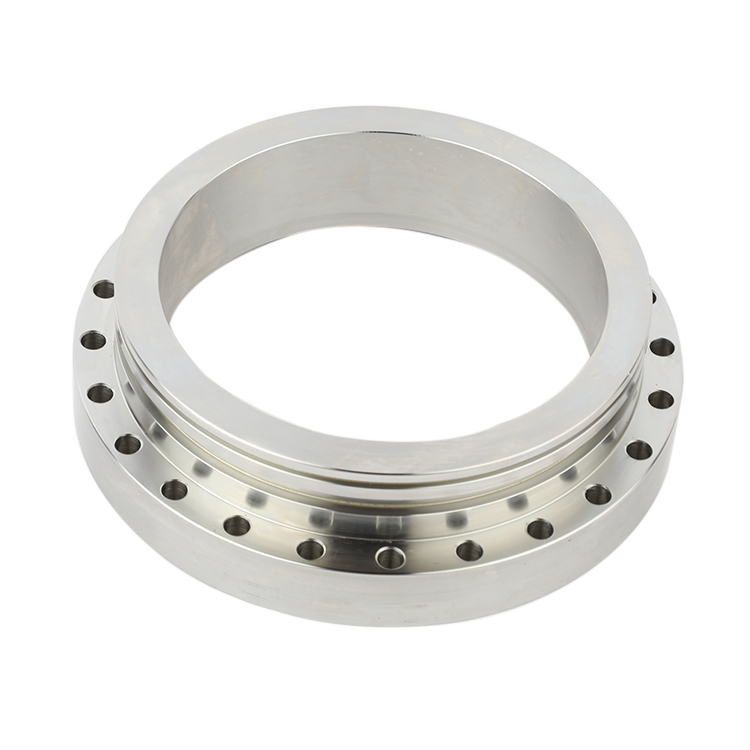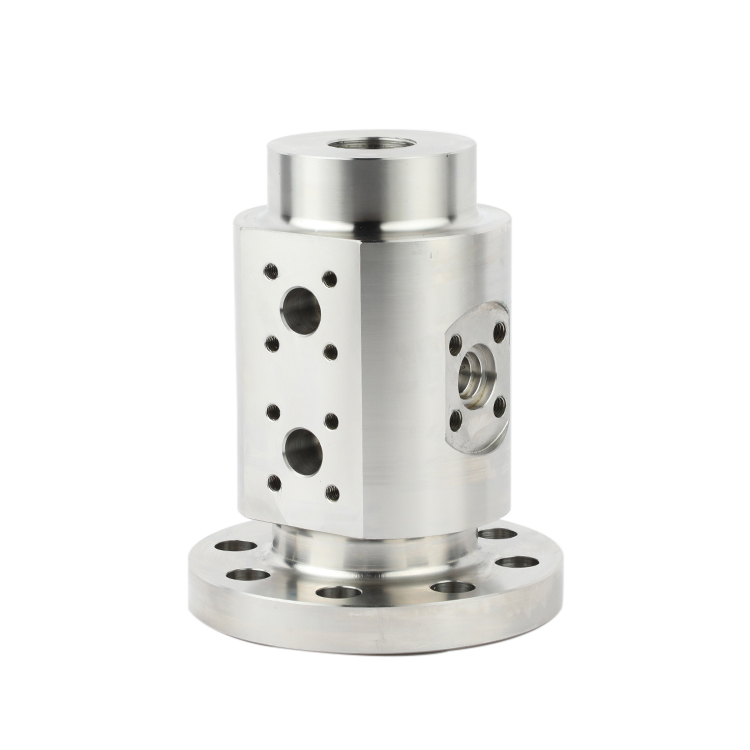

Ball valve body cracks come from five root causes — casting or forging defects that were never detected, heat treatment and hydrogen embrittlement, thermal and pressure cycling in service, mechanical loads the body was not designed for (water hammer, pipe misalignment, over-torqued bolting), and undocumented weld repairs. Prevention works on three levels: specify a sound starting material, inspect the pressure boundary before machining hides the evidence, and control how the valve is installed and operated.
A crack in a valve body is not a maintenance issue. It is a loss-of-containment event waiting for the right pressure and temperature. That is why the question is worth answering properly: not “how do we fix the crack” but “which stage of the process let it exist in the first place.”

Almost every crack begins at a stress concentration: a fillet radius that is too tight, a section change between the flange and the body wall, a thread root, a weld toe, or a machining mark left by a dull tool. The stress raiser does not create the crack, but it decides where the crack appears once the material or the load gives it a reason.
In practice, the reasons cluster into five groups. Each one has a different signature and a different prevention strategy.
| Root cause | Typical crack location | Prevention |
|---|---|---|
| Casting defects (shrinkage porosity, hot tears, cold shuts) | Heavy section transitions, boss-to-wall junctions, seat pocket walls | Riser and gating design, radiography or UT on critical sections |
| Forging defects (laps, bursts, inclusions) | Flange-to-body transition, near the bore | Adequate reduction ratio, UT on billet, magnetic particle after forging |
| Heat treatment and hydrogen embrittlement | Hardened zones, plated threads, weld heat-affected zones | Correct tempering, baking after plating, hardness control per NACE |
| Thermal and pressure fatigue | Body wall at the cavity, seat pocket roots | Generous fillets, wall thickness verification, cycling analysis |
| Mechanical overload | Flange hub, body joint bolts, stem area | Pipe support, correct bolt torque, surge protection |
Casting is still the most economical route for complex body shapes, and it is also the route that hides defects best. Shrinkage porosity forms where the last metal to solidify has nowhere to draw feed metal from — typically at heavy section junctions and around the seat pocket. A hot tear forms while the casting is cooling, when the outer skin is rigid and the interior is still contracting.
Neither defect has to be large to matter. A shrinkage cavity that intersects the bore becomes a leak path at pressure; a hot tear at a fillet becomes a crack once the body is stressed by line load or thermal cycling. Both can pass a visual inspection and even a low-pressure air test.
Radiography and ultrasonic testing are the only reliable ways to find them, and they need to be applied to the right sections. Shooting a film of a uniform wall proves very little; shooting the section transitions and the seat pocket walls is what catches the defects that matter. Our guide to how casting quality affects pressure ratings covers the acceptance criteria in more detail.
Forged bodies avoid casting porosity but introduce their own failure modes. Laps form when folded metal is forged into the surface; bursts appear at the ends of the billet; non-metallic inclusions act as crack initiators under fatigue. A forging with an inadequate reduction ratio retains the cast structure of the original ingot, which defeats the purpose of forging. Ultrasonic inspection of the billet before forging and magnetic particle inspection after forging are the standard controls.

Heat treatment is supposed to improve toughness. Done incorrectly, it does the opposite: an incomplete temper leaves a hard, brittle martensitic structure; a rapid quench on a complex section creates residual stresses that later relieve themselves as cracks; and a normalizing cycle that is too slow can leave a coarse grain structure with poor impact resistance.
Hydrogen embrittlement is a separate and frequently missed mechanism. High-strength steels absorb hydrogen during pickling, electroplating and some welding processes. The hydrogen diffuses to stress concentrators and causes delayed cracking — often days or weeks after the part was plated, which is why a body can pass its factory test and crack in the warehouse.
The controls are well established: bake high-strength parts within a defined window after plating, avoid electroplating on hardness above about 32 HRC where possible, and specify hardness limits for sour service in accordance with NACE MR0175 / ISO 15156. For wet H2S duty, hardness control is not optional — it is the difference between a body that survives and one that cracks in the heat-affected zone of a weld repair.
Fatigue cracks start where cyclic stress meets a stress raiser. In a valve body, that is usually the root of a seat pocket, the transition from the bore to the body cavity, or the fillet between the flange hub and the body wall.
Pressure fatigue comes from cycling between shut-in and flowing conditions, or from pressure pulsation in reciprocating services. Thermal fatigue comes from rapid temperature swings — steam tracing that is switched on and off, cryogenic lines that are cooled too quickly, or a body that is heated on one side and cooled on the other.
The design answer is a generous fillet radius and a verified wall thickness. The wall thickness calculation gives the static margin but says nothing about the local stress concentration, which is why a body can meet ASME B16.34 minimum wall and still crack at a sharp internal corner. Machining practice matters here too: a tool mark left in a fillet is a miniature stress raiser, and polishing or blending that corner is a genuine fatigue improvement, not cosmetic work.
Many “body cracks” are not material failures at all. They are installation and operation failures that the body simply reports.
Water hammer and pressure surge. A fast-closing valve in a long line can produce a pressure spike several times the working pressure. The body may survive the spike, but the flange hub or a casting defect may not.
Pipe misalignment. Pulling flanges together with bolts puts a permanent bending moment into the body wall. The crack appears months later at the flange-to-body transition.
Over-torqued body joint bolts. In split body designs, excessive bolt preload crushes the gasket and loads the joint face beyond its design stress, especially when the bolts are tightened in a poor sequence.
Unsupported weight. A large valve hanging on unsupported pipe transfers its weight into the body as bending stress. Big trunnion valves need their own support.
Thermal shock. Injecting cold water into a hot body, or steam into a cold one, produces a transient gradient that can exceed the material’s thermal shock resistance.
Weld repair of casting defects is normal practice in the valve industry — but only under a qualified procedure. An undocumented repair is the single most common source of unexpected cracking, because three things are usually missing: preheat, a qualified welding procedure, and post-weld inspection.
A repair without preheat on a medium-carbon or low-alloy steel creates a hard, crack-susceptible heat-affected zone. A repair without post-weld heat treatment leaves residual stress that adds to the service stress. A repair without magnetic particle or penetrant inspection afterwards leaves the possibility that the repair itself cracked while cooling.
For buyers, the practical requirement is simple: ask for the weld repair map, the WPS/PQR reference, the welder qualification, and the post-repair NDT report. If a supplier cannot produce those documents, assume the repairs exist but are not controlled.
Get a body that arrives with its inspection paperwork
GOTEB supplies ball valve bodies with material certificates traceable to heat number, dimensional reports, and NDT records on request. If your application is sour, cryogenic or high-cycle, tell us at RFQ stage — we will propose the inspection plan, hardness limits and test pressure before the casting is poured.
Different methods find different defects. Using only one is how cracks get missed.
| Method | Finds | Limitation |
|---|---|---|
| Visual (VT) | Open cracks, corrosion, mechanical damage | Cannot see tight or subsurface cracks |
| Dye penetrant (PT) | Surface-breaking cracks in any material | Only surface; requires clean, dry surface |
| Magnetic particle (MT) | Surface and near-surface cracks in ferromagnetic steel | Not applicable to austenitic stainless |
| Ultrasonic (UT) | Internal defects, wall thickness, laminations | Operator-dependent; geometry makes some zones unscannable |
| Radiography (RT) | Porosity, shrinkage, inclusions in castings and welds | Poor at detecting tight planar cracks perpendicular to the beam |
| Hydrostatic shell test | Through-wall defects and leak paths | Proves containment only; does not size or locate a defect |

First, stop treating it as a cosmetic issue. Any crack in a pressure boundary should be evaluated against three questions: does it penetrate the wall, is it growing, and what is the local stress state?
A surface crack outside the sealing area that is confirmed shallow can sometimes be blended out and re-inspected, provided the remaining wall still satisfies the minimum thickness for the pressure class. Cracks at fillets, in weld heat-affected zones, or anywhere the wall is already at minimum should be treated as cause for replacement.
Excavation and weld repair is acceptable only with a qualified procedure, preheat, controlled interpass temperature, and full NDT after welding — and only if the base material’s toughness and hardness limits allow it. On sour service or high-strength bodies, repair is usually the wrong answer.
Specify the manufacturing route (cast, forged, or forged-and-machined) and the applicable material standard.
Require radiography or ultrasonic testing on section transitions and seat pocket walls, not just on a uniform wall section.
Require magnetic particle or penetrant testing after machining on ferromagnetic bodies, and after any weld repair.
Require material certificates with heat numbers traceable to the NDT and test reports.
Require hardness testing for sour service, with acceptance limits per NACE MR0175 / ISO 15156.
Require a weld repair map with WPS/PQR references and post-repair NDT reports.
Specify the shell test pressure and duration, and a seat test at both low and rated pressure.
Verify wall thickness at the cavity and at the flange transition, not only at the bore.
If you are comparing manufacturing routes for a corrosive or high-cycle application, the trade-offs are set out in cast vs forged ball valve body. The full production sequence, including where each inspection belongs, is covered in how a ball valve body is manufactured.
What causes cracks in cast ball valve bodies?
The most common causes are shrinkage porosity at heavy section junctions, hot tears formed during cooling, and cold shuts where two metal fronts met without fusing. All three concentrate stress and can propagate into cracks under pressure or thermal cycling. Radiography and ultrasonic testing at the section transitions are the only reliable way to find them before machining.
Can a cracked ball valve body be welded?
Only under a qualified weld repair procedure with preheat, controlled interpass temperature, post-weld heat treatment where required, and full NDT afterwards. Cracks in weld heat-affected zones of high-strength or sour service bodies should generally not be repaired, because the repaired zone will have the same hardness and hydrogen susceptibility that caused the original crack.
How do I know if a crack is from manufacturing or from service?
Look at the fracture surface and the location. Manufacturing cracks usually follow a casting or forging feature and show oxidation or scale inside the crack faces. Service cracks initiate at a stress raiser, show fatigue beach marks or a fresh brittle surface, and are often associated with evidence of overload such as pipe misalignment, water hammer damage or thermal discolouration.
Does a hydrostatic test prove a body has no cracks?
No. A hydrostatic shell test proves the body contains pressure at the test pressure for the test duration. A tight crack that is not through-wall, or one that is held closed by compressive residual stress, can pass the test and grow later in service. That is why NDT is a separate requirement from pressure testing.
Why do some bodies crack only after months in service?
Delayed cracking is typical of hydrogen embrittlement and of fatigue. Hydrogen absorbed during plating or welding diffuses slowly to stress concentrators and causes cracking days to weeks later. Fatigue cracks grow a small amount with each pressure or thermal cycle, so the failure appears long after the initiating condition.
What wall thickness is required to prevent cracking?
Minimum wall thickness is set by the pressure class and material allowable stress, typically per ASME B16.34 for valve bodies. That calculation prevents gross plastic collapse, not fatigue cracking at a stress concentration. Local geometry — fillet radius, section transitions, machining marks — determines whether the body cracks below the calculated burst pressure.


 Optimized by Seraphinite Accelerator